Choosing a supplier should not be based on one question:
“Who gave us the lowest price?”
Two factories may quote almost identical products, yet one may have stronger quality systems, better production capacity, faster communication, more suitable equipment, and significantly lower sourcing risk.
The challenge is that supplier evaluation involves many variables at the same time.
A factory may offer excellent pricing but weak quality control. Another may produce an outstanding sample but have insufficient capacity. A third may look professional online while outsourcing most of the manufacturing.
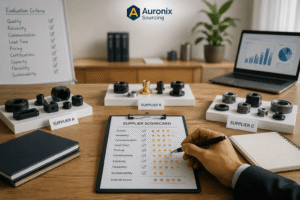
This is why professional importers can use a supplier scoring system.
Instead of choosing based on impressions, buyers assign measurable scores to the factors that matter most to their business and compare suppliers using the same criteria.
Why Supplier Scoring Matters
Without a structured system, supplier decisions can become subjective.
A buyer may favor a factory because:
- The salesperson responds quickly
- The quotation looks attractive
- The website appears professional
- The sample looks impressive
These factors can matter, but none proves that the supplier is the best overall manufacturing partner.
A scorecard forces the buyer to evaluate the complete supplier.
It transforms:
“I think Factory A looks better.”
into:
“Factory A scored 84/100 based on our defined supplier requirements.”
That makes the decision easier to explain, review, and repeat.
Start With Your Product Requirements
Before scoring suppliers, define what your business actually needs.
Consider:
- Product specifications
- Materials
- Target quantity
- Required certifications or compliance
- Customization
- Quality expectations
- Target lead time
- Packaging
- Budget
A factory cannot be considered “good” or “bad” in isolation.
It must be evaluated against the requirements of the specific project.
A manufacturer that is excellent for 100,000-unit orders may be completely unsuitable for a startup ordering 2,000 units.
Use Weighted Scoring
Not every supplier criterion deserves equal importance.
For many sourcing projects, quality and manufacturing capability should carry more weight than small differences in unit price.
A practical 100-point scorecard might look like this:
| Category | Weight |
|---|---|
| Manufacturing Capability | 20 |
| Quality Management | 20 |
| Price & Commercial Terms | 15 |
| Sample Performance | 15 |
| Production Capacity & Lead Time | 10 |
| Communication | 10 |
| Supplier Verification | 5 |
| Packaging & Customization | 5 |
| Total | 100 |
The weights should be adjusted for the product.
For a technically complex product, manufacturing capability might deserve 30%.
For a commodity product, commercial terms may receive greater weight.
1. Manufacturing Capability — 20 Points
The first question should be:
Can this supplier reliably manufacture the product you actually need?
Evaluate:
- Relevant machinery
- Production processes
- Technical expertise
- Engineering support
- Tooling capability
- Similar product experience
A factory producing similar products with appropriate equipment may represent less technical risk than a supplier learning the manufacturing process through your order.
Do not confuse general factory size with relevant capability.
Check What Is Actually Manufactured In-House
A supplier may claim:
“We manufacture everything.”
But several important processes may actually be outsourced.
Subcontracting is common and is not automatically a problem.
However, buyers should understand which processes are:
In-house vs. outsourced
because this affects:
- Quality control
- Lead times
- Traceability
- Supply-chain dependency
For strategically important processes, direct factory capability may deserve additional scoring.
2. Quality Management — 20 Points
Quality should usually receive significant weight.
Evaluate how the factory controls quality throughout production.
Useful areas include:
- Incoming material inspection
- In-process quality checks
- Final inspection
- Testing procedures
- Defect handling
- Corrective-action processes
Do not evaluate quality only by asking:
“Do you have good QC?”
Almost every supplier will answer yes.
Look for evidence of how quality is actually managed.
Evaluate Quality Records Where Available
For an existing supplier, historical performance provides stronger evidence than promises.
Track indicators such as:
- Defect rate
- Inspection failures
- Customer complaints
- Rework frequency
- Corrective-action effectiveness
For a new supplier, samples, audits, and production-system evaluation can provide useful evidence.
3. Price and Commercial Terms — 15 Points
Price matters.
But price should be evaluated after confirming that suppliers are quoting comparable products.
Normalize quotations based on:
- Material
- Components
- Quantity
- Packaging
- Customization
- Incoterms
Otherwise, Factory A may appear 12% cheaper simply because it quoted a lower-grade component.
Evaluate More Than Unit Price
Commercial scoring can also consider:
- MOQ
- Tooling costs
- Sample costs
- Payment terms
- Packaging costs
The best commercial supplier is not necessarily the one with the smallest number in the unit-price column.
Evaluate the complete commercial structure.
4. Sample Performance — 15 Points
Samples provide physical evidence of supplier capability.
Create a sample evaluation checklist.
Depending on the product, score:
- Dimensions
- Materials
- Functionality
- Workmanship
- Finish
- Branding
- Packaging
Avoid evaluating samples only through:
“Looks good.”
Measurable sample scoring creates a more useful comparison.
Compare Samples Under the Same Conditions
If three factories provide samples, test them using the same criteria.
For example:
| Requirement | Supplier A | Supplier B | Supplier C |
|---|---|---|---|
| Dimensions | 5/5 | 4/5 | 5/5 |
| Workmanship | 4/5 | 5/5 | 3/5 |
| Functionality | 5/5 | 5/5 | 4/5 |
| Finish | 4/5 | 5/5 | 4/5 |
This makes the evaluation less dependent on first impressions.
5. Production Capacity and Lead Time — 10 Points
A factory can produce an excellent sample and still be the wrong supplier if it cannot handle your order volume.
Evaluate:
- Realistic monthly output
- Current capacity utilization
- Relevant production-line capacity
- Normal lead time
- Peak-season lead time
- Expansion capability
Ask specifically about available capacity during your required production window.
Theoretical maximum capacity is less useful than available capacity.
Verify Capacity Claims
A supplier saying:
“Capacity: 1 million units/month”
does not automatically make that number reliable.
Factory visits or audits can help evaluate:
- Number of machines
- Production lines
- Workforce
- Current utilization
- Bottlenecks
Capacity should make sense relative to the physical manufacturing operation.
6. Communication — 10 Points
Communication quality can significantly influence manufacturing performance.
Evaluate whether the supplier:
- Answers questions clearly
- Responds within reasonable time
- Understands specifications
- Identifies problems early
- Provides useful production updates
Fast replies alone should not receive a perfect score.
A supplier responding:
“Yes friend, no problem.”
within two minutes may be less useful than a supplier taking several hours and returning with a detailed technical answer.
Score the quality of communication, not simply speed.
Test Communication Before Ordering
The RFQ and sample process provide excellent opportunities to evaluate communication.
Ask technical questions.
See whether the supplier:
- Understands them
- Consults engineering
- Provides evidence
- Identifies limitations
A supplier willing to say:
“We need to check this with engineering.”
can sometimes be more trustworthy than one immediately saying yes to everything.
7. Supplier Verification — 5 Points
Before committing significant money, verify that the business is what it claims to be.
Depending on the order and risk level, verification may consider:
- Company information
- Factory location
- Manufacturing activities
- Relevant equipment
- Export experience
- Quality systems
For significant or customized projects, a factory audit or visit can provide additional information.
Supplier verification should happen before large financial commitments whenever practical.
8. Packaging and Customization — 5 Points
For branded products, evaluate whether the supplier can support your requirements involving:
- Logo application
- Private labeling
- Custom colors
- Retail packaging
- Inserts
- Master cartons
A factory with slightly higher unit pricing but stronger customization capability may create better overall value for a brand.
Use a Consistent 1–5 Rating Scale
A simple rating system keeps scoring manageable.
For example:
5 — Excellent
Strong evidence that the supplier exceeds requirements.
4 — Good
Meets requirements with minor concerns.
3 — Acceptable
Meets minimum requirements.
2 — Weak
Important concerns remain.
1 — Poor
Does not adequately meet requirements.
Each rating can then be multiplied by the category weight to calculate the overall supplier score.
Example Supplier Comparison
After completing due diligence, three suppliers might score:
| Category | Supplier A | Supplier B | Supplier C |
|---|---|---|---|
| Manufacturing Capability | 18 | 16 | 13 |
| Quality Management | 17 | 19 | 12 |
| Price & Terms | 12 | 10 | 15 |
| Sample Performance | 13 | 15 | 10 |
| Capacity & Lead Time | 8 | 9 | 7 |
| Communication | 8 | 9 | 6 |
| Verification | 5 | 5 | 4 |
| Packaging & Customization | 4 | 5 | 4 |
| Total | 85/100 | 88/100 | 71/100 |
Supplier C has the strongest price score.
But Supplier B receives the highest overall score because of stronger quality, sample performance, communication, and production capability.
This illustrates why price alone can produce the wrong supplier decision.
Add Pass/Fail Requirements
Not every factor should be averaged into a score.
Some requirements should be non-negotiable.
For example, a supplier might automatically fail qualification if it cannot meet an essential:
- Manufacturing requirement
- Material specification
- Safety requirement
- Regulatory requirement
A very high score in price cannot compensate for inability to manufacture a critical specification.
Use both:
Pass/Fail Gates + Weighted Scorecard
This creates a stronger supplier-selection system.
Watch for Artificially High Scores
A scorecard is only useful if the underlying information is reliable.
Do not give a factory 10/10 for production capacity simply because the salesperson claims enormous output.
Where possible, distinguish between:
Supplier Claim → Documented Evidence → Independently Verified Evidence
The stronger the evidence, the more confidence you can place in the score.
Compare Factories After the Same RFQ
Supplier scoring becomes much more accurate when every factory receives the same RFQ.
If Supplier A quotes 5,000 units with premium packaging while Supplier B quotes 10,000 units with standard packaging, comparing their prices directly is misleading.
Standardize:
- Product specification
- Quantity
- Packaging
- Incoterms
- Quality expectations
Then compare the responses.
Red Flags Should Override the Score
A supplier may achieve a reasonable numerical score but still present a serious warning sign.
Examples could include:
- Refusing reasonable verification
- Unauthorized material substitution
- Inconsistent company information
- Repeatedly changing bank details without credible verification
- Misrepresenting manufacturing capability
Critical red flags should be investigated independently rather than averaged away by strong scores elsewhere.
Do Not Automatically Choose the Highest Score
The scorecard supports judgment—it does not replace it.
Suppose:
Supplier A: 88/100
Supplier B: 86/100
Supplier B may still be strategically preferable if it has unique engineering expertise or better capacity for future growth.
The numerical result should make the decision more disciplined, not mechanical.
Keep a Second Supplier Qualified
The scoring process can also identify a backup manufacturer.
Instead of discarding every factory except the winner, consider keeping the second strongest supplier qualified.
If your primary factory later experiences:
- Capacity problems
- Quality deterioration
- Price increases
- Supply disruption
you already have a credible alternative.
This can substantially reduce sourcing risk.
Update Supplier Scores Over Time
Supplier selection should not end when the first purchase order is placed.
Real production provides better data.
After each order, update relevant scores using actual performance.
Track factors such as:
- On-time delivery
- Defect rates
- Inspection results
- Communication
- Corrective actions
A supplier that originally scored 90/100 may decline over time.
Another may steadily improve.
Build a Supplier Performance History
After multiple orders, replace assumptions with data.
For example:
Order 1: 96% on-time milestones
Order 2: Inspection passed
Order 3: 2.1% defect rate
Order 4: Corrective action completed successfully
Historical performance makes future supplier decisions significantly stronger.
It can also support negotiations.
Score Suppliers by Product, Not Just Company
A factory may be excellent for one product and average for another.
For example, a manufacturer might have outstanding:
- Plastic molding capability
but weak:
- Electronics assembly capability.
Do not assume that because a supplier performs well on Product A, it is automatically the best manufacturer for Product B.
Supplier qualification should consider the specific manufacturing process required.
How Auronix Sourcing Helps Evaluate Suppliers
Auronix Sourcing helps businesses evaluate Chinese manufacturers using more than quotations and online profiles.
Support can include supplier discovery, RFQ management, quotation comparison, supplier verification, factory audits and visits, sample management, manufacturing-capability assessment, commercial negotiation, production-capacity evaluation, quality inspection, packaging coordination, production monitoring, backup supplier development, shipment consolidation, and international shipping coordination.
By comparing suppliers across technical, commercial, quality, and operational criteria, Auronix helps businesses identify manufacturers that offer stronger overall sourcing value—not simply the lowest quoted unit price.
Conclusion
Supplier selection becomes much more reliable when buyers replace intuition with structured evaluation.
A practical approach is:
Define Requirements → Set Pass/Fail Criteria → Send Standardized RFQ → Verify Suppliers → Test Samples → Score Each Factory → Compare Total Value → Select Primary and Backup Suppliers
The goal is not to find the cheapest factory.
It is to identify the supplier offering the strongest combination of manufacturing capability, quality, commercial value, capacity, communication, reliability, and long-term fit.
A supplier scorecard makes those trade-offs visible.
With Auronix Sourcing, businesses can identify, verify, compare, and qualify Chinese manufacturers before committing significant orders—helping turn supplier selection from a price comparison into a disciplined sourcing decision.